Rotating Ceramic Membrane Filtration System Membrane Filtration System (RO/NF/UF/MF)
Processed Cheese Sterilizer Infusion/Injection Sterilizer High Pressure Processing Sterilizer Plate Sterilizer Pilot Sterilizer Tubular Sterilizer
Vacuum Mixing System In-line Blending System Sauce Preparation System Multi-Functional Cooking & Homogenization Tank System​ ​Applications
Enzymatic Hydrolysis & Cooking System Laboratory Vacuum Enzymatic Hydrolysis System
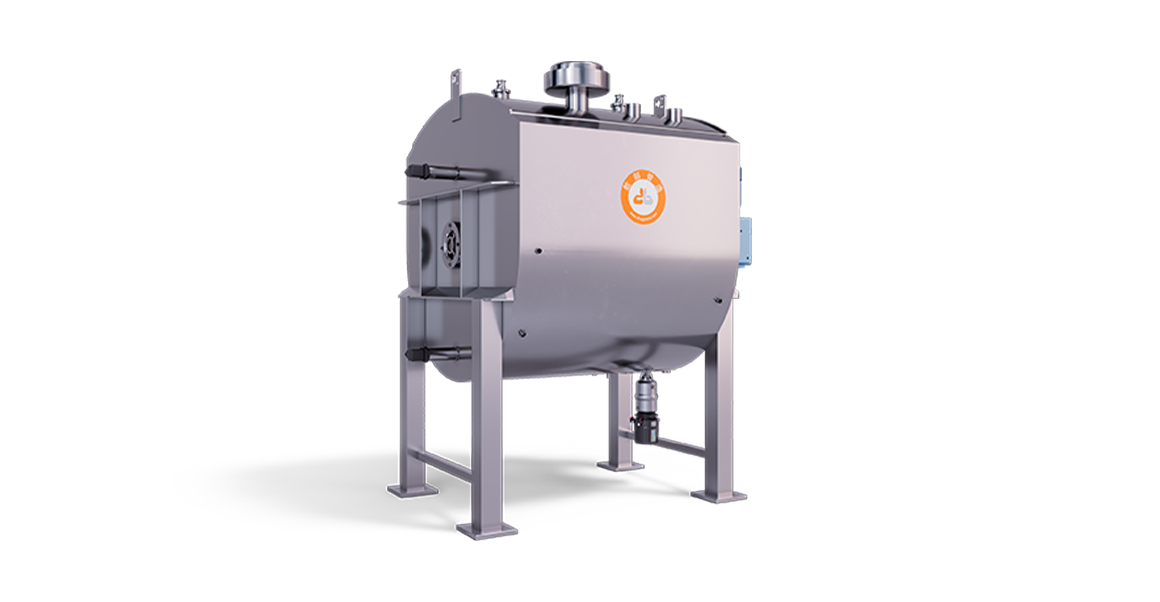
Horizontal Aseptic Tank Horizontal Dual-Agitation System Stainless Steel Storage Tank Horizontal Holding Tank System Aseptic Tank Sauce Storage System


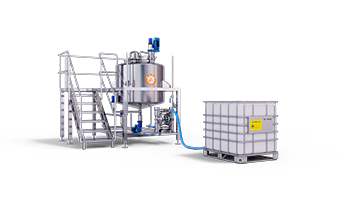
Application:
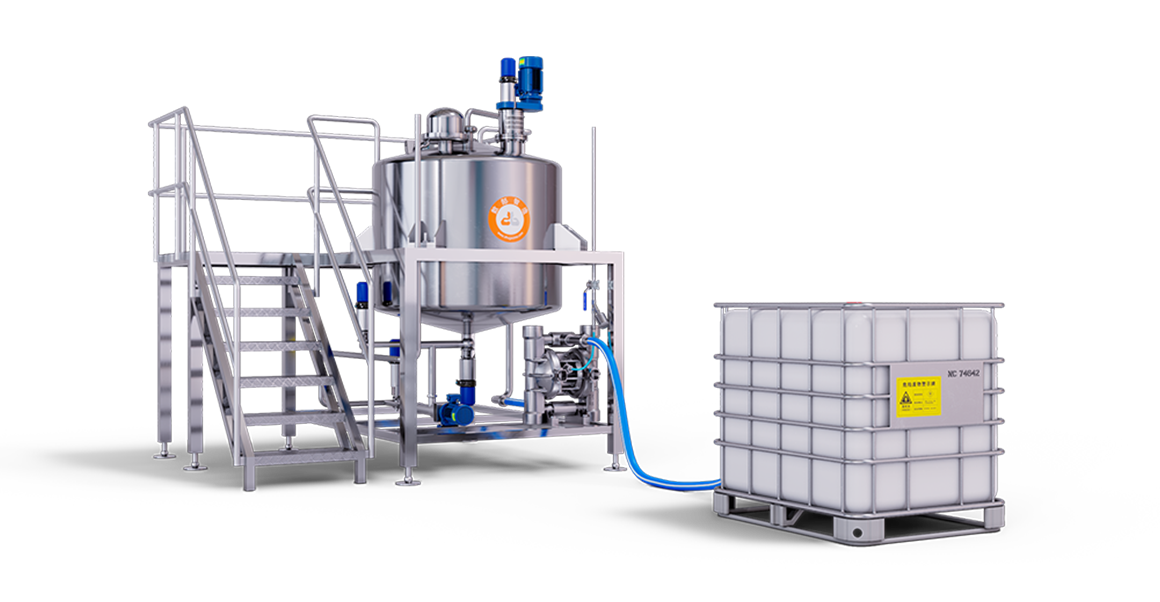
Designed for receiving fluid food ingredients and additives, including oils, syrups, sauces, and liquid vitamins.
Technical Features:
• Customizable tank design based on product characteristics.
• Optional mixing configurations (scraped-wall frame or paddle mixing).
• Anti-foaming feeding process to minimize air entrainment.
• Discharge system: Bottom valve + screw pump for controlled output.
• Optional insulation with jacket options:
Honeycomb jacket
Half-coil jacket
Full jacket
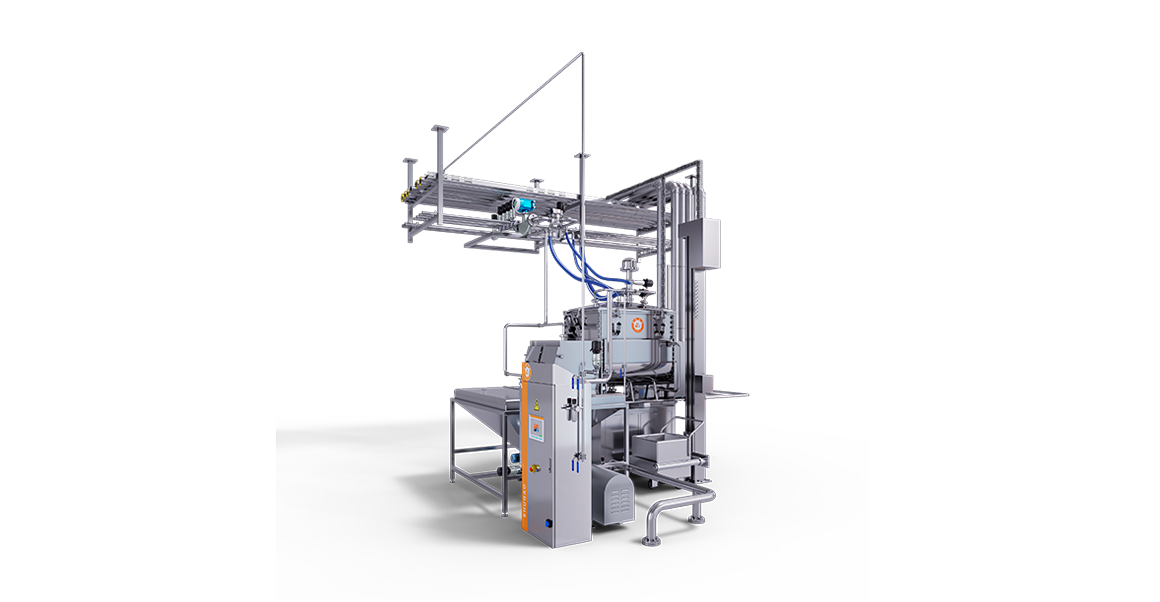
Application:
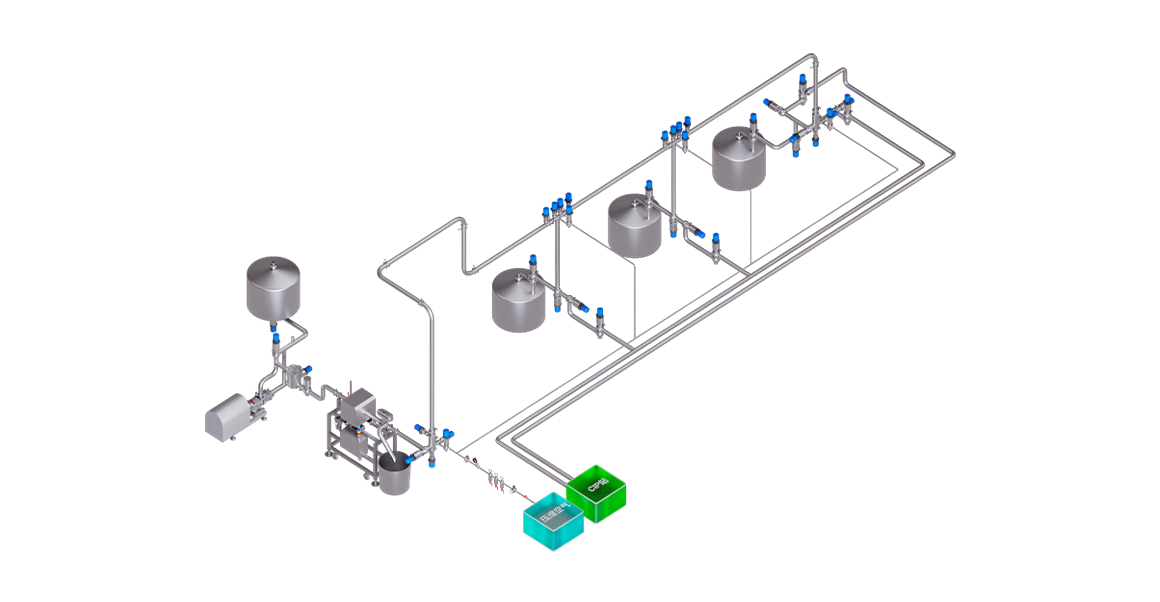
Designed for pipeline maintenance operations using propelled pigs to perform cleaning, product recovery, and phase separation without system disassembly. This process enhances production efficiency, minimizes product waste, and maintains pipeline integrity.
Key Features:
• High-efficiency cleaning: Removes pipeline deposits, contaminants, and residues rapidly
• Non-intrusive operation: Performs cleaning and recovery without pipeline disassembly
• Product recovery: Maximizes yield by recovering residual product
• Customizable design: Adaptable to various pipeline configurations and operational requirements
• Multiple propulsion options:
Product-driven
Gas-propelled
Water-driven
Solvent-based
• Automated operation: Features complete pig launch, transit, and receiving automation
Technical Advantages:
• Reduces equipment downtime significantly
• Improves overall production efficiency
• Minimizes cross-contamination risks
• Lowers cleaning solvent consumption
• Maintains consistent pipeline hygiene standards
Applications
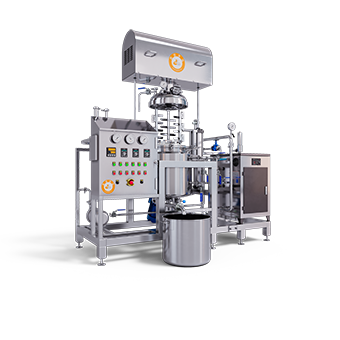
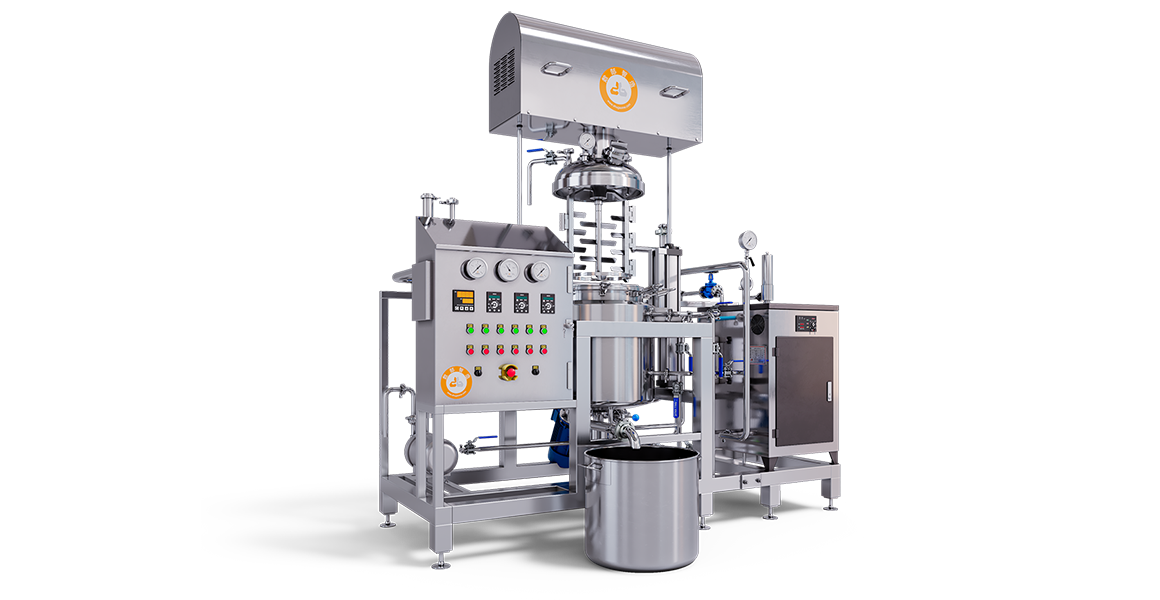
A versatile mixing and heating system designed for R&D in food ingredient processing, capable of handling various viscosities. Ideal for:
• Sauces & dressings (tomato sauce, salad dressing, cheese sauce, mayonnaise)
• High-protein fluid products (medical/special dietary foods)
• Dairy-based formulations (cream cheese, processed cheese, heavy cream)
Tank Capacity: 100L (customizable)
Key Features
• Steam injection heating – Rapid and efficient thermal transfer
• Variable-speed bottom high-shear mixing – Ensures precise, smooth, and uniform blending
• Heating/cooling jacket – Accurate temperature control for fermentation, enzymatic hydrolysis, etc.
• Vacuum chamber (-0.5 bar) – Quickly removes entrapped air during mixing/shearing
• Pressure-rated vessel (121°C capable) – Enables complete sterilization & enzyme deactivation
• Dead-zone-free bottom valve – Prevents material stagnation
• Dual-pneumatic lid opening – Effortless operation
• Top-mounted feeding port – Allows precise small-batch ingredient addition
• Full SS316 stainless steel construction – Higher sanitary standards
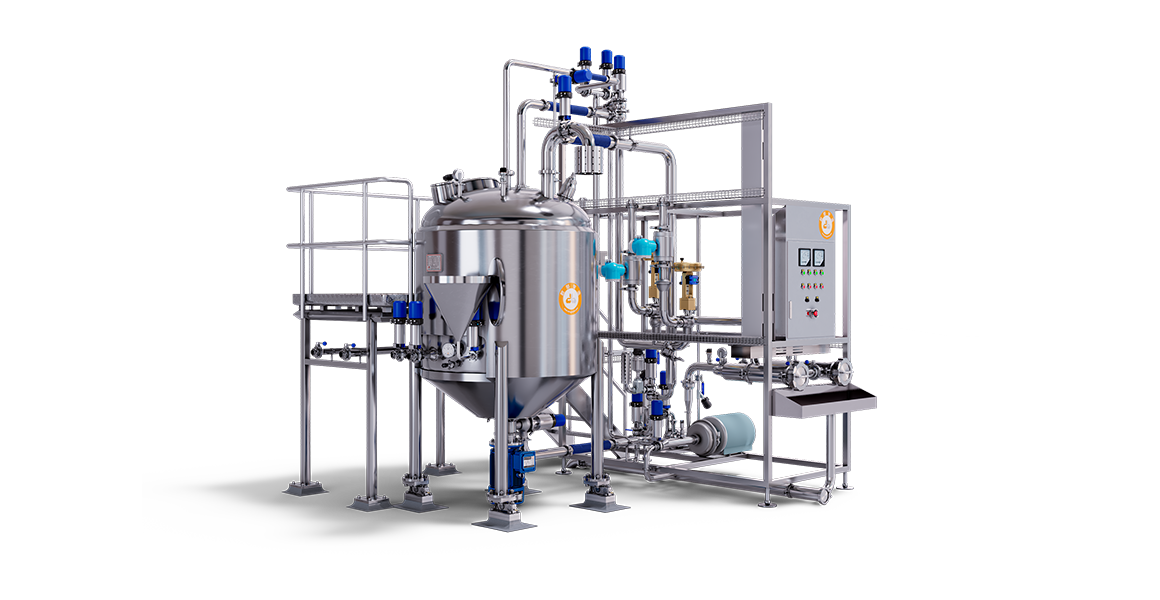
Applications
A fully integrated processing system designed for liquid/semi-liquid food products, supporting:
• Fermentation & enzymatic hydrolysis
• Extraction, mixing, and homogenization
• Sterilization & Maillard reaction control
Key Features
• Bottom-flow material guidance
Adjustable high-shear emulsifier at tank base
Dual coaxial agitators:
• Wall-scraping frame + dual-layer paddles
Anti-foam top feed
Vacuum degassing & material suction
Direct steam injection heating
Pressure-rated vessel (0.5 bar max)
Controlled exhaust with aroma recovery
Segmented heating jacket
Customizable tank configurations
Streamlined exterior protects motor
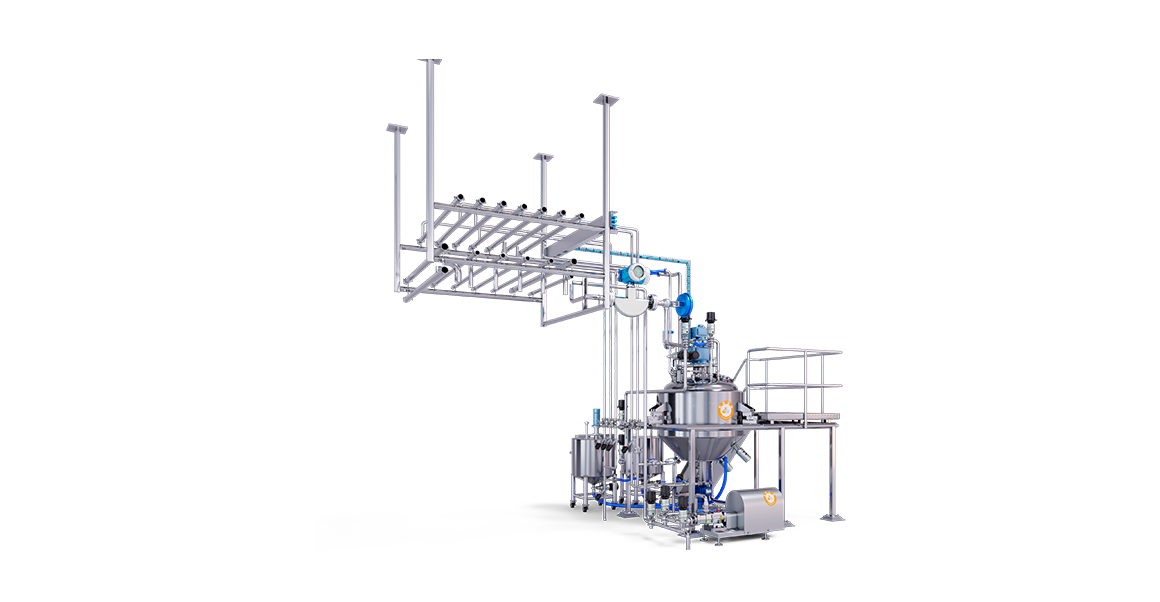
Applications
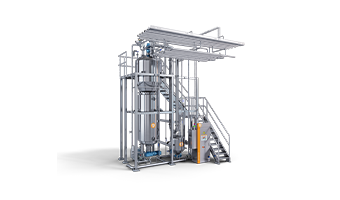
A specialized industrial system designed for sauces, condiments, and food processing, utilizing flash evaporation technology to:
• Rapidly remove moisture & gases
• Concentrate product consistency
• Enhance sterilization & overall quality
Key Features
• High-Efficiency Concentration
• Flash evaporation enables fast water removal, significantly boosting production output.
• Flavor & Nutrient Retention
• Low-temperature process preserves original taste and nutritional value.
• Built-in Sterilization
• High-temperature flash evaporation eliminates microbes, extending shelf life.
• Energy-Saving & Eco-Friendly
• Advanced heat exchange technology reduces energy use and minimizes wastewater.
• Fully Automated Control
• Integrated smart system for hands-off operation and real-time monitoring.
• Customizable Design
• Adaptable configurations to match diverse sauce properties (viscosity, acidity, etc.).
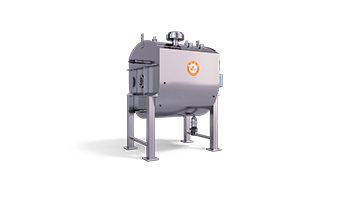
Application:
Designed for temporary storage of high-viscosity or particle-containing materials prior to filling.
Capacity: 300–5,000L (customizable).
Key Features:
• Horizontal mixing design prevents phase separation and particle settling.
• Optional jacketing for thermal control.
• Multi-functional capabilities:
Heating & cooling
Positive-pressure assisted discharge
Applications
Designed for storing viscous materials, as well as intermediate storage and transfer of low-fluidity products.
Capacity: 1,000–30,000 liters
Key Features
• Mixing Options:
• Wall-scraping frame agitator
• Dual helical ribbon agitator with wall-scraping function
• Feeding Methods:
Bottom/side inlet (prevents material mixing)
Top inlet (minimizes foam formation)
• Discharge System:
Feeder + screw pump for controlled material output
• Tank Configurations:
Single-layer, insulated, or jacketed (Miller plate, semi-coil, full jacket)
• Versatility:
Compatible with a wide range of product consistencies
Applications
Primarily designed for pre-packaged foods, semi-liquid foods, pet food, and other viscous, particle-containing materials, supporting:
• Mixing & blending
• Heating & cooling
• Deaeration & vapor release
Key Features
• Automatic top cover opening/closing
• Precision metering (for liquid or powder ingredients)
• Vapor release & deaeration functions
• Accurate temperature control
• Bi-directional agitation (freely switchable rotation)
• Automated loading/unloading with residual material recovery
• CIP (Clean-in-Place) system
• Customizable tank design
• Fully automated control
Application:
Designed for storing various liquids, powders, or liquid mixing applications.
Capacity: 25L – 200,000L (customizable).
Key Features:
• Customizable design based on product requirements.
• Food-grade construction, compliant with hygiene standards.
• Material options: 304/316 stainless steel (special materials available upon request).
• Surface finish: Oil-polished or wire-drawn exterior.
• Mixing options (optional):
Anchor-type
Paddle-type
Scraper-type
High-shear
• Thermal control: Optional insulation or jacket.
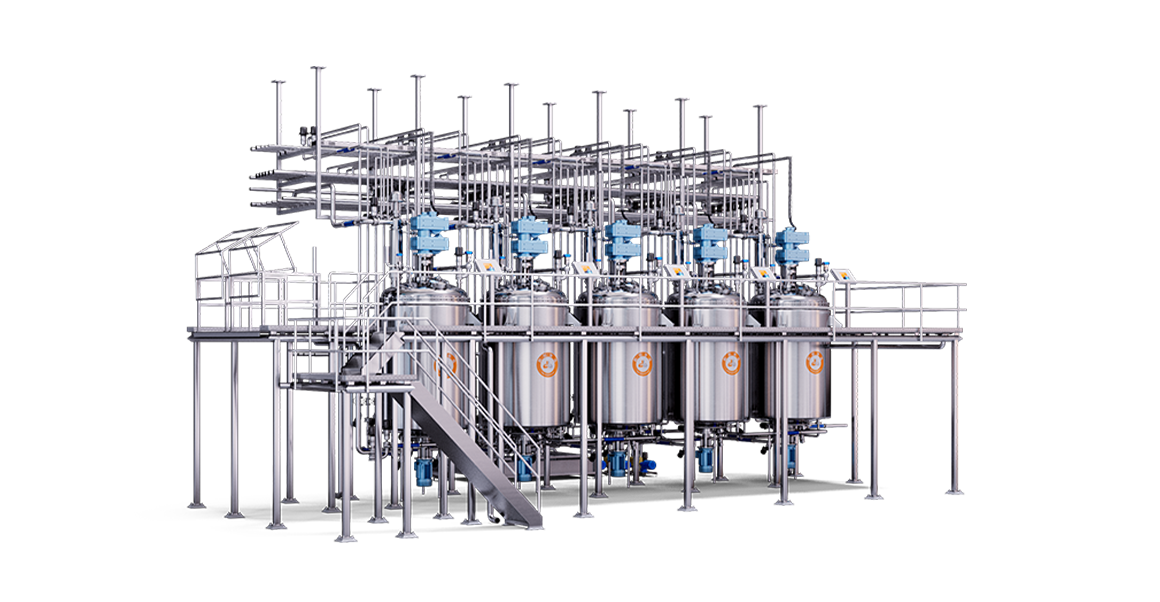
Applications
A versatile solution for mixing, cooking, sterilization, emulsification, rapid cooling, vacuum deaeration, and vacuum concentration across diverse production requirements.
Capacity: 500–3,000 liters
Key Features
• Integrated 5-in-1 Functional Modules:
Cooking/reactor
Weighing
Jacketed temperature control
Positive/negative pressure
Direct steam injection
• Customizable tank design tailored to product specifications
• Dual Agitation System:
Top-mounted coaxial dual agitators
Bottom high-shear homogenizer (1,450/2,900 rpm, with guide impeller)
• Bottom vacuum feeding
• Multi-layer heat/cooling exchange
• Positive-pressure assisted heating & discharge
• Direct steam injection heating
Applications
Designed for sauce formulation, emulsification, and homogenization in food processing.
Key Features
• Vacuum feeding system for precise metering of liquids or powders
• High-shear homogenization unit for uniform texture
• Agitator for consistent mixing
• Heating module for temperature-controlled processing
• Metering pump for accurate ingredient delivery
Applications
A fully automated, high-efficiency mixing solution designed for dairy products, beverages, ice cream, and other food industry applications requiring:
• Powder emulsification
• Hydration
• Standardization
Tank Capacity: 500–10,000 liters
Key Features
• High-shear mixing head ensures rapid dispersion, dissolution, and emulsification of solids in liquids.
• Vacuum deaeration effectively removes air pockets for superior product consistency.
• Hermetically sealed design complies with EHEDG & 3A sanitary standards, guaranteeing product safety.
• Energy-optimized operation with variable frequency drives (VFD) and vacuum systems reduces both running costs and carbon footprint.
• Scalable production from small batches to continuous large-scale output, with customizable solutions.
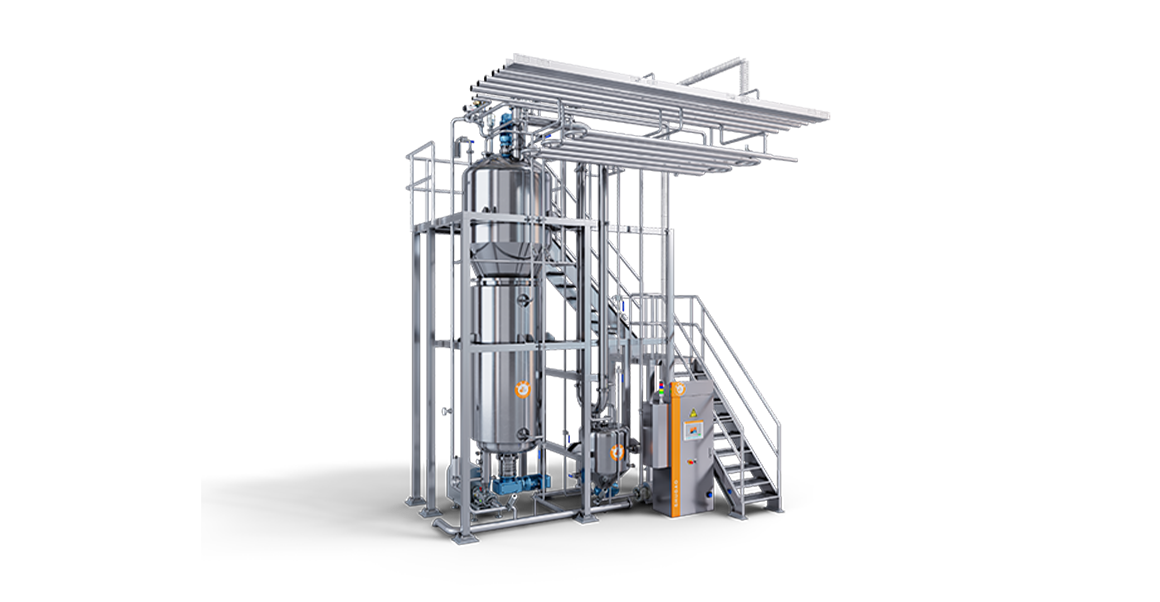
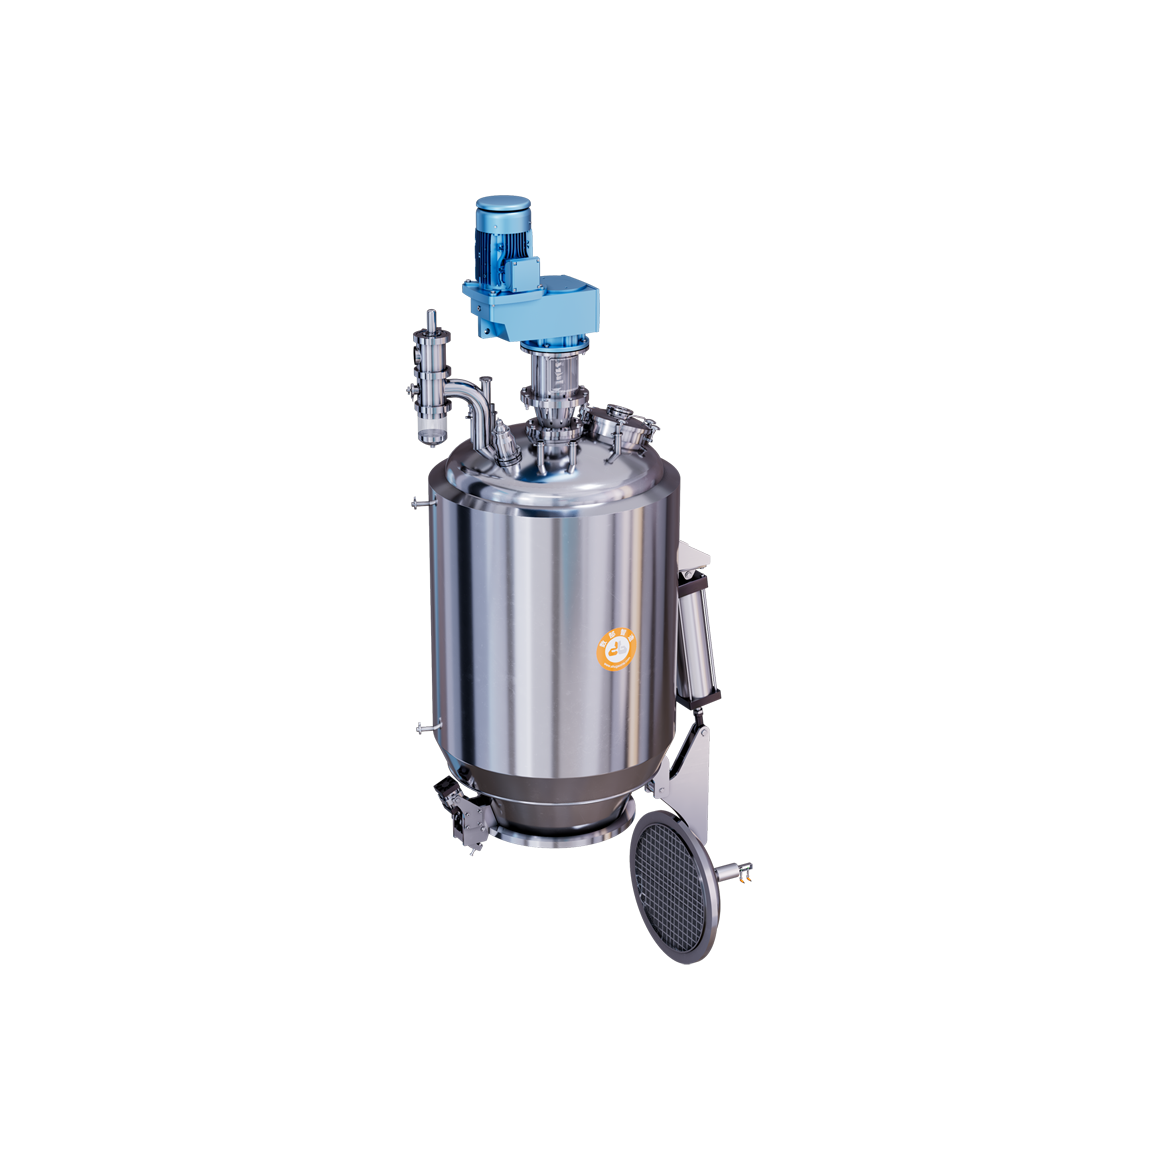
Applications
Designed for atmospheric, positive/negative pressure extraction of:
• Coffee beans
• Tea leaves
• Herbal materials
Capacity: 500–6,000 liters
Key Features
• Multi-functional processing:
Direct steam injection heating
Rapid cooling
Vacuum deaeration & concentration
• Customizable Configurations
Tank structures: Positive-cone, mushroom, straight-tube, inverted-cone
Extraction methods: Top-load basket type / bottom-discharge dump type
Jacket options: Full/half/dimpled configurations
• Advanced Thermal Control
Multi-layer heat exchange system
Positive-pressure assisted heating/discharge
Integrated aroma recovery
• All 316L stainless steel contact surfaces, EHEDG compliant design.
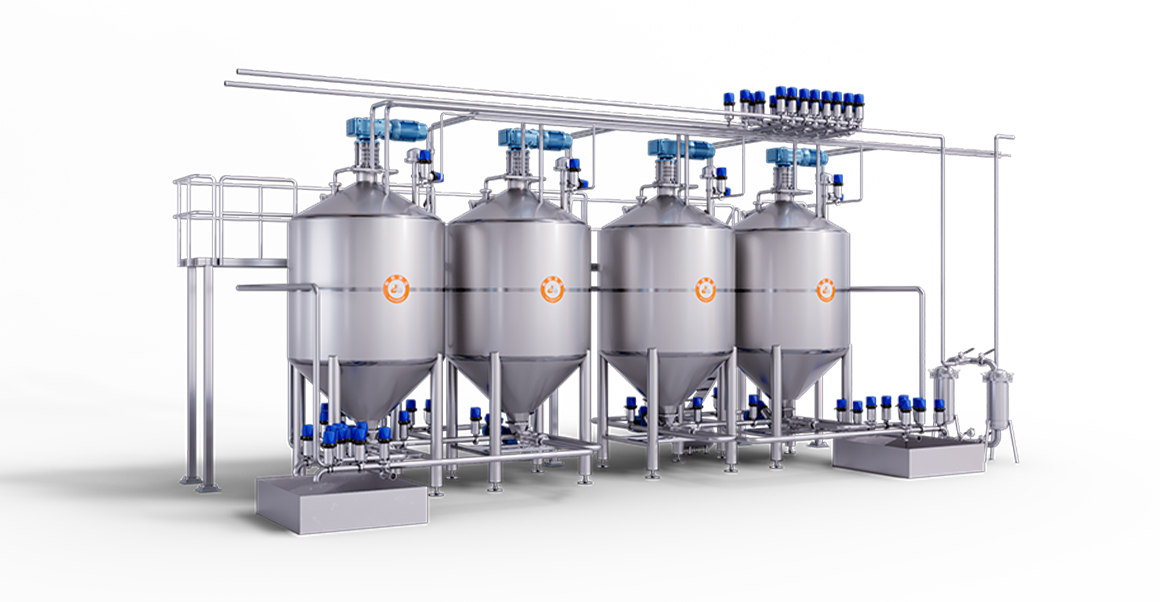
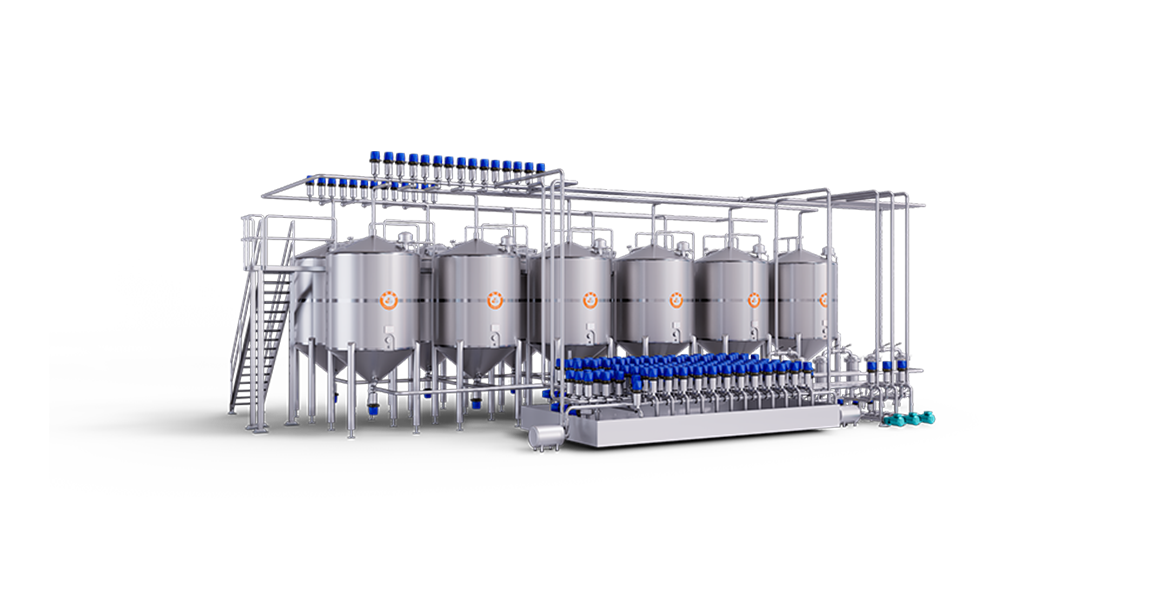
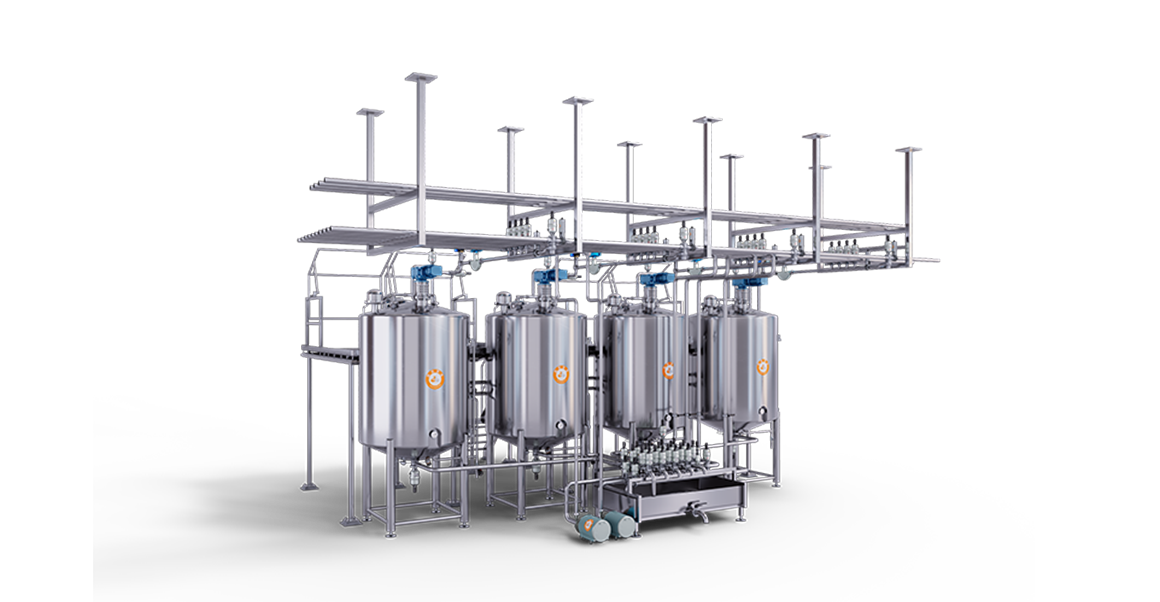
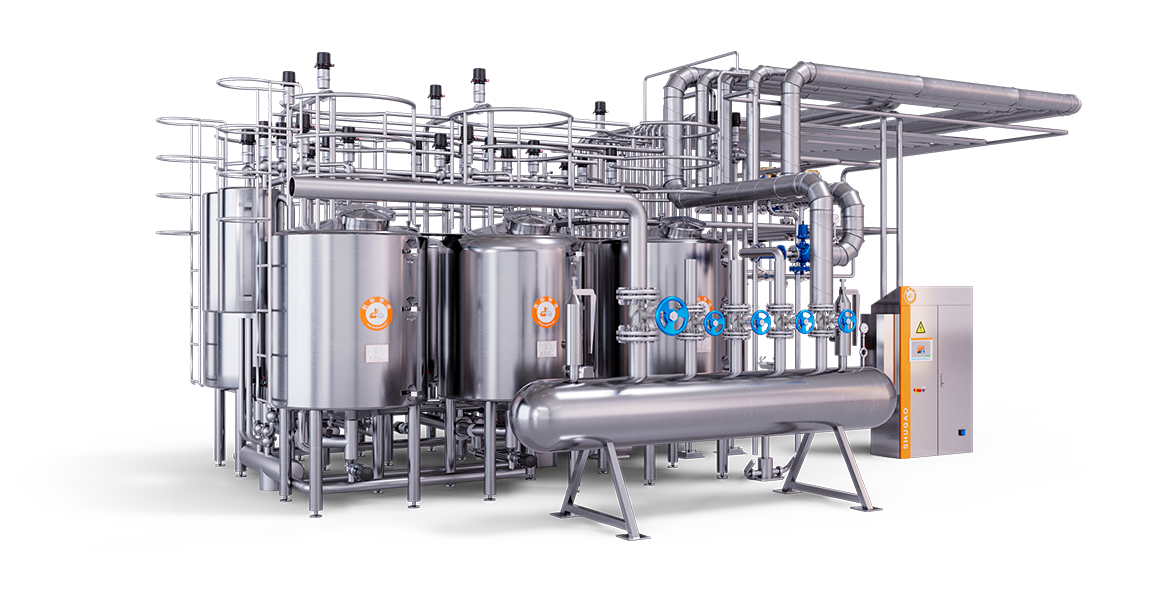
Application:
Designed for automated cleaning of tanks, equipment, and pipelines in food processing applications.
Key Features:
• Precision cleaning control with automated management of:
Cleaning solution temperature, flow rate, and concentration
Water parameters
Cycle duration
• Optimized cleaning cycles minimize downtime while ensuring thorough cleaning
• Dual control capability with synchronized operation between central control room and field stations
• Optional configurations:
Independent small-tank cleaning cycle
High-concentration cleaning solution discharge system

sale@shugaome.com